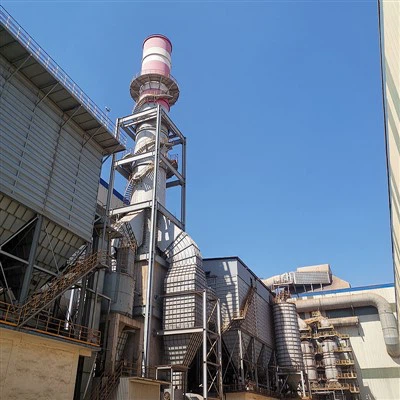
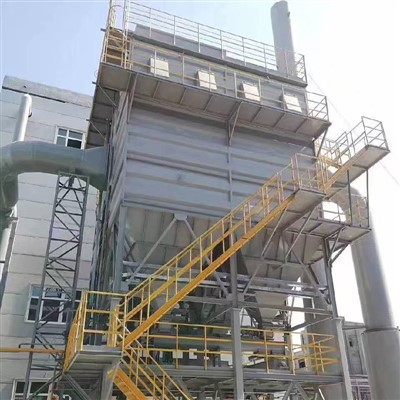
Our Large Scale Reverse-Air Baghouse Dust Collectors offer an industrial-grade solution for extreme-duty air pollution control. Designed for applications with exceptionally high air volume and heavy dust loading, these systems feature a compartmentalized design with offline reverse-air cleaning. By integrating a modular structure and a highly reliable control system, these units are ideal for large-scale flue gas treatment projects in power generation, metallurgy, and cement production. As a leading product among baghouse dust collector manufacturers, we ensure these Large Scale Reverse-Air Baghouse Dust Collectors deliver unmatched reliability and performance under demanding conditions.


Product Parameters
|
Parameter |
Specification |
|
Product Model |
Large Scale Reverse-Air Baghouse Dust Collectors |
|
Air Volume Capacity |
300,000 – 2,000,000 m³/h |
|
Filtration Area |
10,000 – 80,000 m² |
|
Filtration Velocity |
0.4 – 0.8 m/min |
|
Operating Temperature |
Up to 280°C+ |
|
System Resistance |
1200 – 1800 Pa |
|
Number of Compartments |
6 – 24 (Independently Operable) |
|
Cleaning Method |
Offline Reverse-Air (Low Pressure, High Flow) |
|
Control System |
PLC + HMI with Remote Diagnostics |
Main Applications
This equipment is the optimal choice for large-scale dust control in:
Power Generation
Flue gas treatment for coal-fired and biomass boilers, as well as waste incineration plants.
Metallurgy
Dedusting of sintering machines, blast furnaces, and non-ferrous metal smelting furnaces.
Cement & Building Materials
Ideally suited as a cement dust collector for kiln tail gases, raw mills, and clinker cooler exhausts. It also functions as an effective cement silo dust collector for large storage systems.
Heavy Chemical Industry
Treatment of tail gases from carbon black reactors, titanium dioxide calciners, and fertilizer production lines.
Frequently Asked Questions (FAQ)
Hot Tags: large scale reverse-air baghouse dust collectors, China large scale reverse-air baghouse dust collectors manufacturers, suppliers, factory, industrial dust collector, Dust Collector Bag, electrostatic precipitators for power plants, central machinery portable dust collector, dust extraction systems, handler manufacturing dust collectors